Using Advanced Plasma ALD Technology to Achieve Conformal Deposition on High Aspect Ratio Features, Control over Film Properties and Selective Area Growth
We are very pleased to present the research projects of two PhD students from Eindhoven University of Technology (TU/e). As a leading university in Engineering Science and Technology, TU/e has been working on innovative process technologies dedicated to advancing the industrial application of Atomic Layer Deposition (ALD), an advanced deposition technique that allows for ultra-thin films to be deposited with atomic-level thickness control.
After 15 years of partnership between Oxford Instruments Plasma Technology and Eindhoven University of Technology, we continue to push the boundaries of ALD research and development which is one of the most rapidly evolving techniques used in many applications of nanofabrication. Both research students, Karsten Arts and Marc Merkx, have used Oxford Instruments' FlexAL ALD system featuring a remote inductively coupled plasma source, enabling high quality deposition.
The Vital Role of Film Conformality
Karsten Arts has focused on the influence of ions on film conformality during the plasma-enhanced ALD process. Film conformality can be challenging to achieve, especially in 3D nanostructures with deep trenches and high aspect ratios, with the thickness uniformity of the deposited film being very important for many applications.
These deep trenches are challenging to cover by uniform films using conventional methods of deposition. In contrast, ALD is renowned for its ability to cover 3D nanostructured surfaces with extremely high aspect ratio and simultaneously achieve precise control in material properties. The ability to obtain highly conformal coatings with controlled thickness have made ALD popular for many nanotechnology applications.
Previously, Karsten and the team at TU/e have found out how to cover extremely deep aspect ratio features by optimising the process conditions (e.g. the temperature of the substrates and the plasma pressures). The reached aspect ratio with plasma ALD of silicon oxide (SiO2) and titanium oxide (TiO2) can approach 1000 which is far beyond what was previously expected to be achievable by plasma ALD (up to 50 or so).
In his current research paper, Karsten demonstrates how to achieve TiO2 film conformality by using plasma-assisted atomic layer deposition with Oxford Instruments' FlexAL system and low-energy ions on vertical trench nanostructures and microscopic cavity structures.
As Karsten has observed, "The influence of ions can be significant even under mild plasma conditions and when using a grounded substrate"1. With plasma present, the ions are accelerated vertically, bombarding the horizontal surfaces, but they are not interacting with the TiO2 on vertical surfaces (the sidewalls). "This influence is verified to significantly affect the film conformality obtained on 3D nanostructures"1, as the film does not grow with uniformity in the nanostructure.
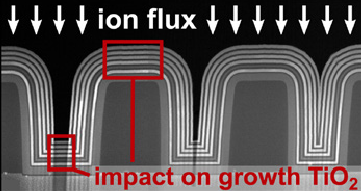
Fig. 1 — Image of different trenches, with layers of TiO2 (white layers), SiO2 (dark grey layers), and a single layer of Al2O3, all grown by plasma ALD using an Oxford Instruments' FlexAL ALD system.However, under the right plasma conditions and energy of ions, Karsten and the research team have accomplished deposition of TiO2 with high film conformality and process reproducibility. The ion energy and flux can be tuned to influence the film properties on horizontal surfaces when desired.
Oxford Instruments' FlexAL ALD system provides an RF-biased electrode option available for control of film properties and allows low process temperatures to enable high-quality deposition on more temperature-sensitive materials such as polymers. FlexAL enables researchers to precisely control the ion energy and flux of ions which is a crucial factor in influencing the film growth of silicon oxide and titanium dioxide.
Researching Area-Selective ALD
Marc Merkx has focused on understanding the capabilities of area-selective processes during atomic layer deposition (ALD). The field of area-selective ALD has gained interest in the semiconductor industry, as it gives more process control at the atomic scale and can reduce fabrication errors by replacing top-down approaches by self-aligned bottom-up approaches.
Area-selective deposition during ALD enables production to reduce lithography steps, meaning a more simplified process, and elimination of alignment issues that might be caused after lithography.
Marc and the research team achieved highly selective growth of titanium nitride (TiN), an important conductive material for application as diffusion barrier and contact material for instance. TiN was deposited with Oxford Instruments' FlexAL ALD system, achieving high selectivity on dielectric surfaces (SiO2, Al2O3) without using any patterning.
The ALD cycle of TiN started by exposing the substrate to "small inhibitor molecules that selectively adsorb on the non-growth area"2 which prevent the precursor adsorption and ultimately the precursor molecules are absorbed selectively only on the growth area. After applying plasma on the substrate, the adsorbed precursors are converted into a nitride. The final step of this process uses a remote plasma with substrate bias to remove any impurities that have been caused during the process, ensuring that only high-quality nitride is deposited on the substrate.
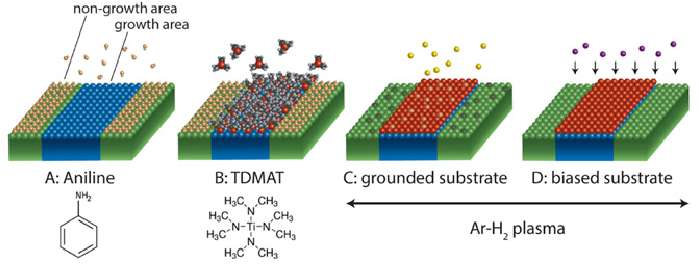
Fig. 2 — Schematic illustration of the ABCD-type ALD cycle.
Area-selective ALD can been achieved even on very small surface features (e.g. 50 nm) and yields "high-quality TiN films in terms of conductivity and oxygen impurity levels"2. TiN growth around 6 nanometres has been achieved with the FlexAL ALD system on SiO2 and Al2O3 surfaces with high selectivity.
As Marc states, "One of the greatest advantages of FlexAL system is the plasma capabilities". Oxford Instruments' FlexAL offers maximum flexibility in the choice of precursors, process gases and hardware features and provides remote plasma for low damage plasma ALD combined with thermal ALD in one deposition chamber.
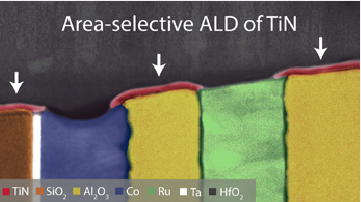
Fig. 3 — Area-selective ALD of TiN.
The Revolution of Atomic Layer Deposition
Both research papers have made great contributions to the understanding of fundamental research of ALD. Advancements and new research projects about film conformality and area-selective ALD can give great insights that could improve the control and capability of nanofabrication in many applications.
With more than 6000 process recipes in our database, Oxford Instruments Plasma Technology will continue to support R&D and production customers and apply our expertise to further develop their fabrication processes to achieve novel research and maximise device performance.
References
- Impact of Ions on Film Conformality and Crystallinity during Plasma-Assisted Atomic Layer Deposition of TiO2. Karsten Arts, Harvey Thepass, Marcel A. Verheijen, Riikka L. Puurunen, Wilhelmus M. M. Kessels, and Harm C. M. Knoops. Chemistry of Materials
- Article ASAP. DOI: 10.1021/acs.chemmater.1c00781
- Area-Selective Atomic Layer Deposition of TiN Using Aromatic Inhibitor Molecules for Metal/Dielectric Selectivity. Marc J. M. Merkx, Sander Vlaanderen, Tahsin Faraz, Marcel A. Verheijen, Wilhelmus M. M. Kessels, and Adriaan J. M. Mackus. Chemistry of Materials
- 2020 32 (18), 7788–7795. DOI: 10.1021/acs.chemmater.0c02370